Choosing the best Ready Concrete Mixer in 2026 means looking beyond advertised capacity. A machine must deliver consistent batches, fit the worksite, and withstand daily loading, washing, and travel. A GCCA Concrete Future report estimates that roughly 14 billion cubic metres of concrete are used worldwide each year. That scale makes reliability more than a sales feature.
Small details matter. Check drum capacity, discharge speed, water control, maintenance access, and parts availability. On a busy site, a slow discharge can hold up a crew; dried concrete around the drum can turn routine cleaning into lost time. The right choice also depends on the job: a truck-mounted mixer, a stationary unit, and a small-site mixer solve different problems. They should not be ranked as if they were interchangeable.
Professor Karen Scrivener, a leading cement and concrete researcher, has described concrete as “the most widely used material in the world after water.” The IEA’s 2023 cement-sector tracking report puts global cement production at about 4.1 billion tonnes in 2022. Those figures offer context, not a buying verdict. There is no universal winner. Published capacity figures may also differ from useful output under real working conditions, so buyers should verify them with operating data. A careful comparison weighs build quality, service support, total ownership cost, and the actual mix being produced. Some specifications look impressive on paper. That is not enough.
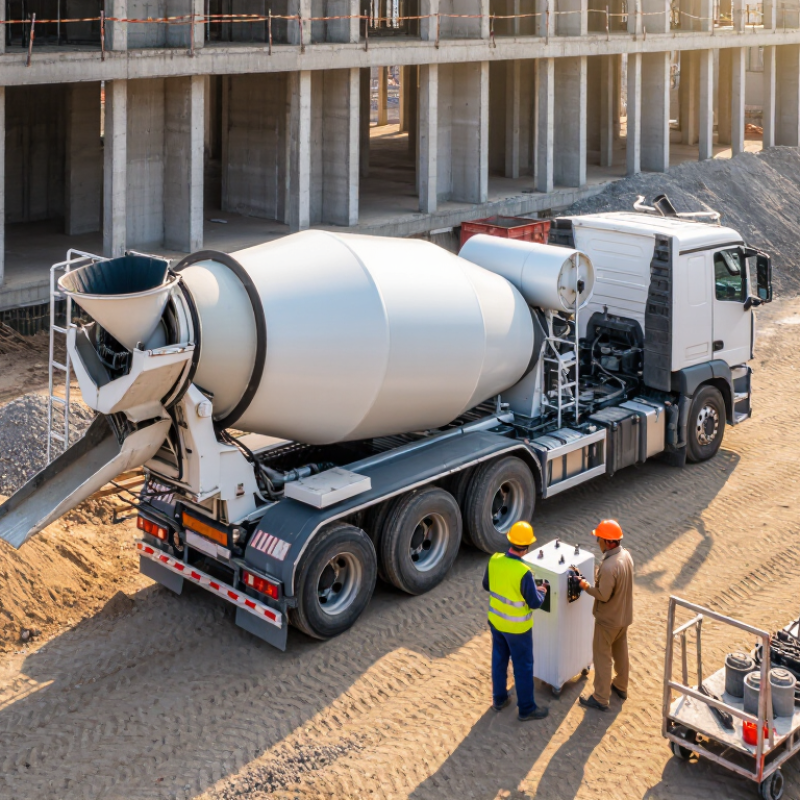
A ready-mixed concrete mixer does more than carry concrete to a jobsite. In a truck mixer, rotating blades blend the batch or keep it moving during delivery. The goal is concrete that remains workable and reasonably uniform from the plant to the chute. Look inside the drum: worn blades, hardened buildup, or uneven rotation can affect how well the load moves and discharges.
ASTM C94/C94M covers ready-mixed concrete production and delivery, including requirements for mixing, transportation, and discharge. It also clarifies what the purchaser and producer need to specify and verify. The standard does not make every mixer equally suitable, nor does the truck determine concrete strength. Mix proportions, materials, batching, and handling all matter. Details count.
On site, check the delivery ticket, note the arrival time, and observe whether the concrete flows consistently as it leaves the drum. If water or another adjustment is proposed, follow the applicable project requirements and document the change. A clean drum matters. So does maintenance. Still, a mixer can look sound and perform poorly under load; inspection alone is not proof of uniform mixing. The actual mixture and delivery conditions deserve attention.
Choosing a ready concrete mixer starts with where the ingredients meet. In a drum system, materials blend inside a rotating truck drum, either during travel or on site. It suits familiar delivery routines, but traffic and waiting can affect how much workable time remains. Central-mix concrete is blended at a plant before transport. This gives the batch a controlled, consistent mixing process, while delivery timing matters because the concrete continues to age in the truck. No system wins every site.
A volumetric mixer carries cement, aggregates, and water separately, then combines them at the job site. Operators can adjust the mix or produce only the amount needed, which helps with remote locations and phased pours. Calibration matters: aggregate moisture or a poorly set water rate can change the result. Small adjustments are possible. For a tight urban pour, truck access and discharge speed may matter more than on-site flexibility. For scattered repairs, producing fresh concrete as needed may reduce leftover material. The choice is not always obvious; a flexible setup can demand more operator attention, and a highly controlled plant batch still depends on reliable delivery. Compare site access, haul distance, pour size, and quality-control needs before deciding.
| Comparison factor | Drum mixer truck | Volumetric mixer truck | Central-mix system |
|---|---|---|---|
| Where mixing happens | Concrete is usually batched at a plant, then mixed or agitated in the truck’s rotating drum during transit. | Separate ingredients are carried in compartments and proportioned and mixed by the truck at the jobsite as concrete is discharged. | Concrete is mixed in a stationary plant mixer before it is loaded into a delivery truck. |
| Typical best fit | Conventional ready-mix deliveries where a plant can supply the required mix and the site can receive a full truckload. | Variable-volume, remote, or intermittent jobs where producing only the quantity needed can reduce leftover concrete. | Projects that prioritize consistent, thoroughly mixed concrete and have access to a suitable central batching plant and delivery network. |
| Batch-size flexibility | Generally delivered in truck-sized loads; ordering smaller quantities may be possible, subject to supplier terms and minimum-load charges. | Can typically produce concrete in measured increments during discharge, subject to the machine’s capacity and ingredient supply. | Plant batches can be controlled to specified quantities, but delivery scheduling and truck capacity still affect how much reaches the site at one time. |
| Mix consistency and control | Performance depends on plant batching, adequate drum mixing or agitation, delivery time, and proper handling at the site. | Onboard metering enables production adjustments at the site; accurate calibration, material moisture management, and operator practice are important. | A stationary mixer can provide controlled mixing cycles; consistency still depends on plant quality control, materials, and operating procedures. |
| Time and delivery considerations | Delivery timing matters because the concrete begins hydrating after water and cement are combined; allowable time and handling depend on the mix, conditions, and applicable requirements. | Mixing at discharge can reduce the time mixed concrete spends in transit, but travel, setup, and material replenishment still affect job scheduling. | Plant mixing supports planned production, but the mixed concrete still needs timely transport, placement, and finishing. |
| Waste and leftover potential | A mismatch between ordered load size and actual placement needs can leave surplus concrete; careful estimating helps limit waste. | Producing only the quantity required can help limit unused mixed concrete, though excess raw materials and washout still require management. | Central production can be planned in batches, but leftover concrete may occur if quantities, delivery timing, or site conditions change. |
| Site and infrastructure needs | Requires truck access, a safe discharge area, and a nearby supplier with the requested mix and delivery availability. | Requires truck access plus sufficient room for operation and access to the water and materials carried or supplied for production. | Requires a batching plant, plant operations, and delivery vehicles; the jobsite itself needs access for concrete trucks and placement equipment. |
| Main advantages | Widely used delivery method; straightforward for standard orders when a ready-mix plant is accessible. | Flexible production at the point of use and the ability to adjust output to changing placement needs, within equipment limits. | Mixing takes place in a dedicated plant mixer, allowing controlled batching and mixing before delivery. |
| Main limitations | Dependent on plant location, delivery schedules, and the time available for transport and placement. | Requires skilled operation and maintenance; production rate and available mix designs depend on the machine and its materials. | Requires plant infrastructure and coordinated dispatch; it may be less convenient where plant access or delivery capacity is limited. |
| Best choice in 2026 | Best for routine pours with dependable plant access and predictable load requirements. | Best for changing quantities, isolated jobs, or work where limiting leftover mixed concrete is a priority. | Best when a nearby plant and coordinated delivery can support a steady supply of concrete mixed under controlled plant conditions. |
Note: Equipment capacities, production rates, delivery practices, and mix requirements vary by configuration, supplier, jurisdiction, and project. Confirm specifications, testing, and applicable concrete standards before ordering.
ASTM C94/C94M’s 70–100-revolution benchmark gives ready-mixed concrete a practical mixing check. The count refers to drum revolutions at mixing speed after materials have been added. Too few may leave uneven color or pockets of dry cement. Too many can increase wear and may affect concrete properties, depending on the mix.
Watch the load, not just the counter. A properly charged drum should turn steadily, while the concrete folds through the center rather than merely riding the wall. That movement matters. Still, revolution count alone cannot prove uniformity. Slump, air content, temperature, and properly collected samples offer useful checks at delivery. Site conditions can also change the picture.
The best mixer is not automatically the one with the largest drum or fastest cycle. Capacity, blade condition, load size, and reliable speed control all matter. A small detail counts: hardened material on a blade can disrupt flow. I would treat 70–100 revolutions as a benchmark, not a guarantee. Project specifications and the applicable ASTM edition should guide the actual procedure, especially when a mix behaves unusually.
What Is the Best Ready Concrete Mixer in 2026?
Choosing a ready concrete mixer starts with matching capacity to your actual jobs. A large drum may look efficient, but small pours can leave material unused. Check usable batch capacity, not just the advertised drum volume. Then compare rated output with your expected hourly demand. Output figures can assume ideal loading and nonstop operation. Real sites rarely run that smoothly. Short pauses add up.
Power and batch accuracy matter just as much. Confirm the mixer’s power requirements match the site, including voltage, phase, and available supply. For mobile work, consider fuel use and access to refueling. Ask how the system measures water and aggregates, and whether operators can calibrate it. Even a small measurement error can change concrete consistency. I would also inspect access panels and cleaning points; these are easy to overlook during a showroom visit.
Tips: Bring a typical job’s batch size and schedule when comparing models. Ask for a demonstration using your materials, if possible. Watch the loading sequence, check the controls, and note cleanup time. Don’t rely on one output number. Real conditions can be messier.
Compare representative mixer capacities by estimated practical output. These are generic planning examples, not standardized ratings or product specifications.
| Nominal batch capacity | Estimated practical output* | Illustrative installed mixer power |
|---|---|---|
| 1.0 m³ | 30–45 m³/h | About 37 kW |
| 1.5 m³ | 45–68 m³/h | About 44 kW |
| 2.0 m³ | 60–90 m³/h | About 60 kW |
How to compare: Output depends on the full batching cycle, mix design, and operating conditions—not mixer capacity alone. The output ranges above assume roughly 60–90 seconds per cycle and 75% effective utilization. Verify motor ratings and weigh-system performance against the specific plant design and applicable standards. Batching tolerances are commonly specified around ±1% for cement and water and ±2% for aggregates; confirm the governing requirements for your project.
The best ready concrete mixer in 2026 depends less on headline capacity than on the work it must do. For small pours, a compact mixer can reduce wasted material and maneuver more easily around tight sites. Larger projects may need greater drum capacity and steady loading access. Match the mixer to typical batch sizes, not just the biggest pour on the schedule. Small jobs differ.
Delivery distance changes the choice. Concrete can lose workability while sitting in traffic, so consider route length, congestion, site access, and unloading delays. A mixer that suits a nearby project may be less practical on a long, stop-and-go route. Ask suppliers how their dispatch plans account for travel time and changing site conditions. Distance changes everything. A capacity calculation helps, but it can still overlook a narrow entrance or a slow crew. Check those details before committing.
Maintenance affects availability and operating costs. Inspect the drum, blades, hydraulic lines, tires, and washout arrangements on a regular schedule. Ask whether replacement parts and qualified service are accessible where the mixer will operate. Review maintenance records when assessing a used vehicle, and look for uneven wear or signs of neglected cleaning. The checklist is useful, though it cannot predict every breakdown. Real operating conditions matter: dusty roads, frequent short trips, and repeated loading can all shape service needs.